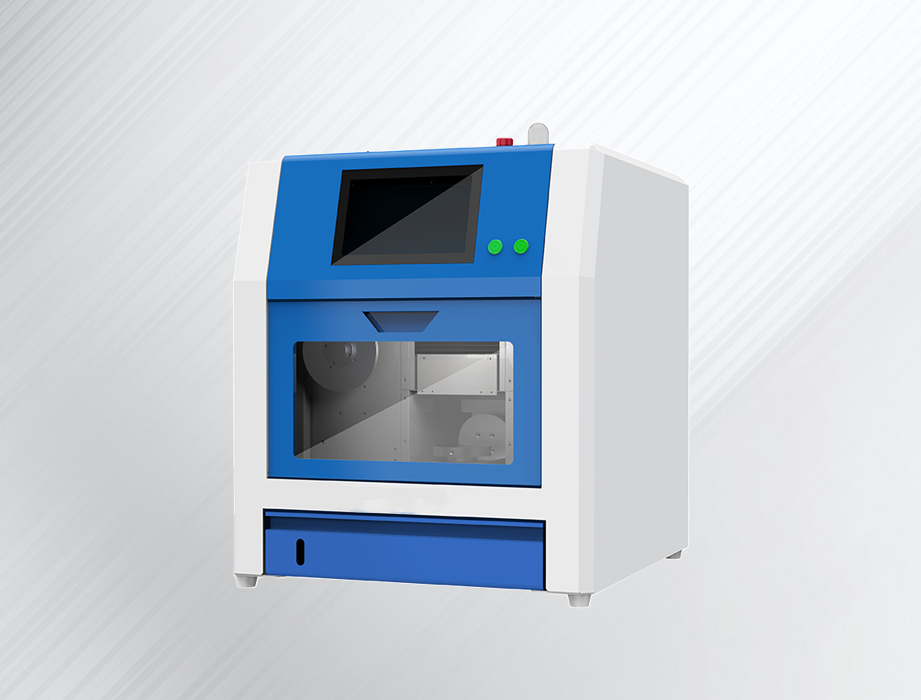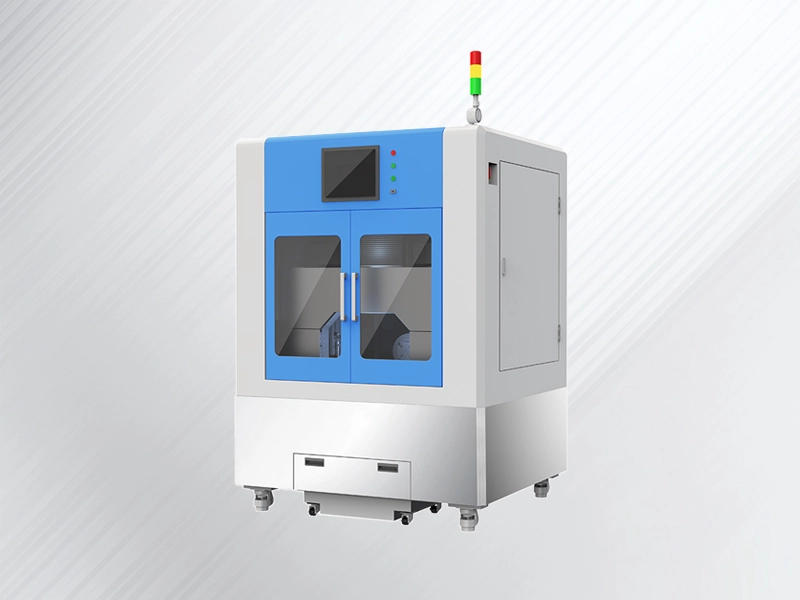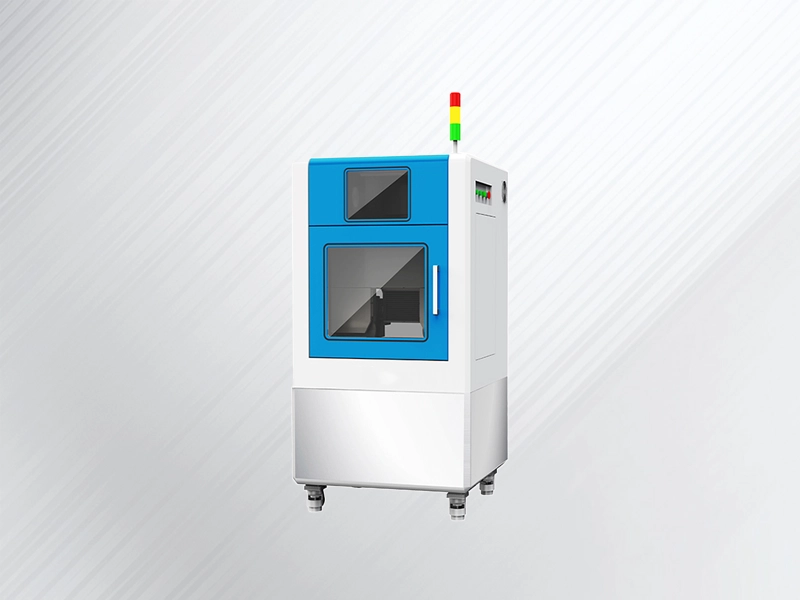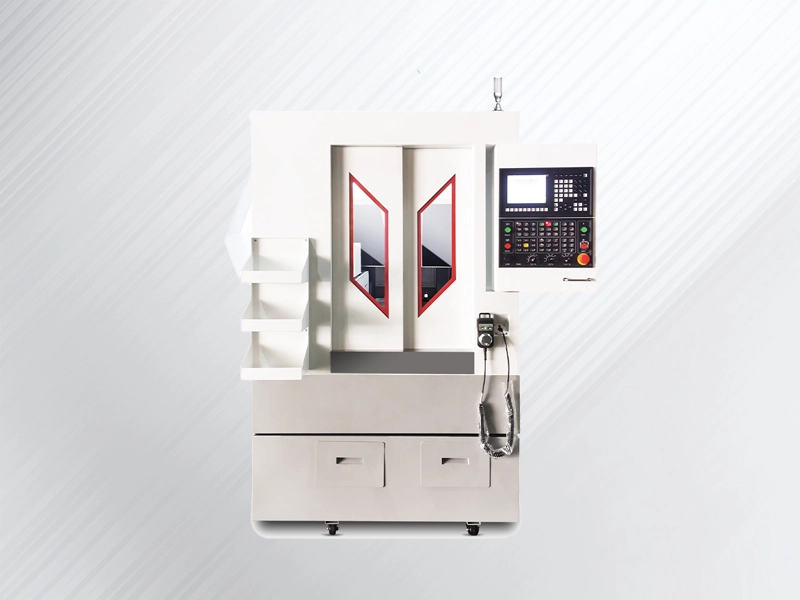
Açıklama
Avantajlar ve Özellikler
Parametre
ürün parametre
| Parametre | Özellikler |
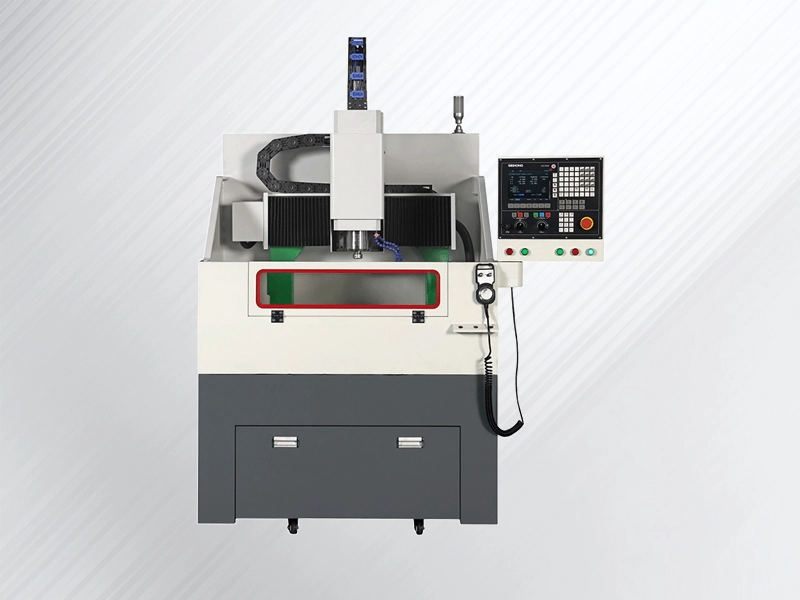
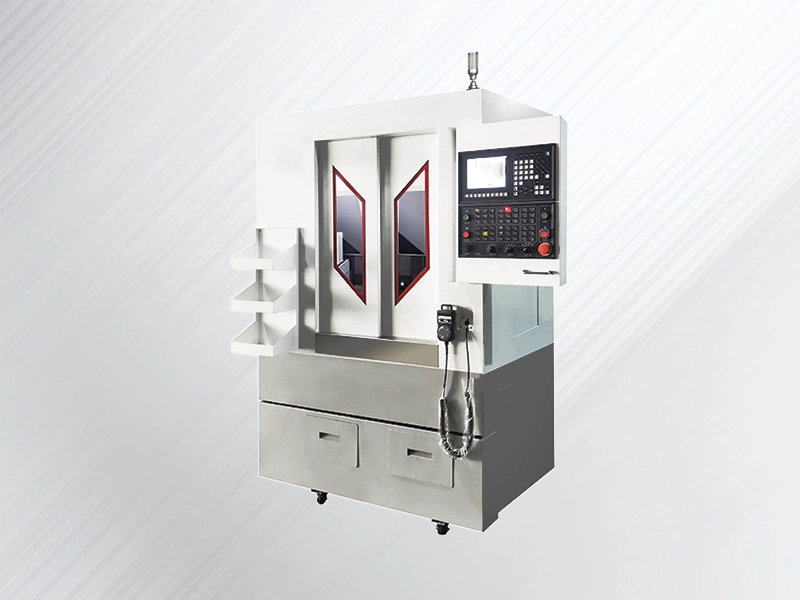
| Takım tezgahı sac metal muhafaza tipi | Tamamen su geçirmez ve toz geçirmez |
| X, Y, Z hareket mesafesi (mm) | 600x500x280 |
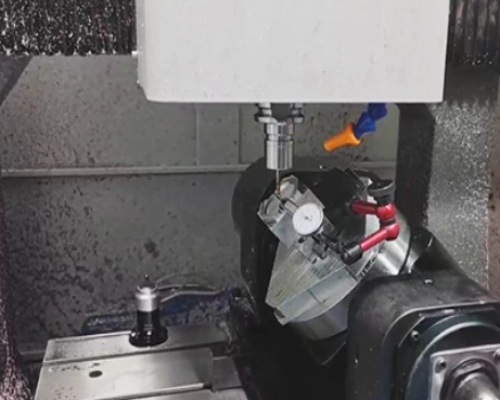
| Maximum workpiece size that can be machined on five axes (mm) | 210x210x155 (Custom sizes available at higher prices) |
| Çalışma masasının boyutları (mm) | 600 × 500 |
| Portal genişliği (mm) | 685 |
| Mil pensi boyutları (mm) | 100/110/Diğer |
| Takım tezgahının boyutları (uzunluk, genişlik, yükseklik) (mm) | 1440x1630x2140 |
| doğrusal kılavuz | HIWIN Taiwan ve Yintai Taiwan'dan H sınıfı kılavuz raylar. |
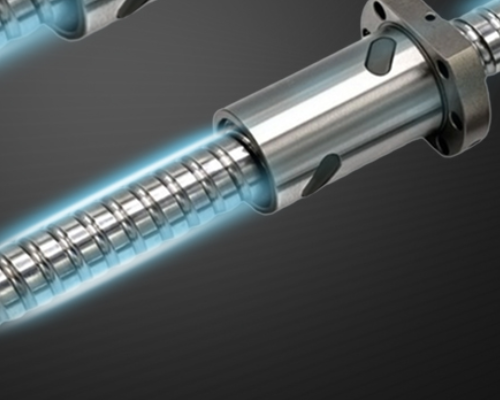
| Sürücü vidası | C5 sınıfı Tayvan TBI taşlanmış kurşun vidası |
| Üç eksenli kılavuz ray boyutları (mm) | 25, 25, 25 |
| Üç eksenli kurşun vida (mm) | 25, 25, 25 |
| Vida aralığı | 10 |
| X, Y, Z axis positioning accuracy (mm) | ± 0.005 |
| Fourth and fifth axis positioning accuracy (mm) | ± 0.006 |
| X, Y, Z axis repeatability (mm) | ± 0.003 |
| Fourth and fifth axis repeatability (mm) | ± 0.005 |
| Üç eksenli kurşun vidalı rulman | Alman IBC |
| Four-axis and five-axis motor power (W) | 750+400 (1100+750 optional) |
| Origin of four- and five-axis reducers | Imported from Japan |
| Güç kaynağı voltajı (V) | 380/220 |
| İş mili gücü (kW) | 5.5 (7.5 isteğe bağlı) |
| iğ | Otomatik takım değiştirici elektrikli iş mili |
| Kolu tipi | BT30 (optional ISO20/ISO25) |
| Takım dergisi | 8 bıçaklı disk şarjörü |
| iş mili hızı | 24000 (36000 isteğe bağlı) |
| Mil soğutma yöntemi | Su soğutma (yağ soğutma opsiyonel) |
| Spindle nose to fifth axis rotary table (mm) | 155 |
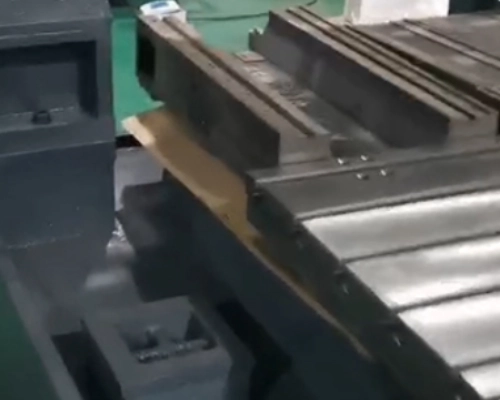
| Makine yatağı malzemesi | Tamamı dökme demir (HT300) |
| bağlama | Diğerleri |
| Dahili koruma | Saint-Jet steel protective/accordion protective |
| Uçağın ağırlığı (kg) | 1750 |
| İsteğe bağlı yapılandırma | |
| doğrusal kılavuz | Tayvan HIWIN ve Tayvan Yintai P sınıfı kılavuz rayları |
| Sürücü vidası | C3 sınıfı Tayvan TBI taşlama vidası |
| Vida aralığı | 5 |
| işletim sistemi | Weihong/Baoyuan/Huazhong/Xindai, vb. |
| Beş eksenli fonksiyon | RTCP blade tip following function |
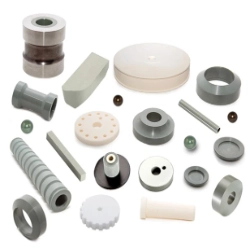
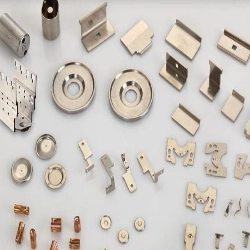
Uygulama
SSS
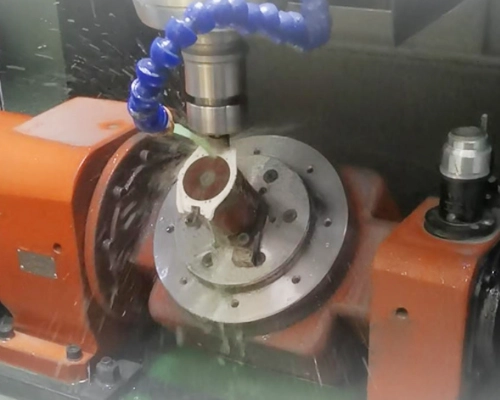
A 5 axis engraving and milling machine moves a cutting tool or workpiece across five different axes simultaneously: three linear axes (X, Y, Z) and two rotational axes (typically A, B, or C). This allows the tool to approach the workpiece from virtually any direction, enabling complex geometries, deep cavities, and undercuts to be machined in a single setup . This reduces setup time and improves accuracy compared to traditional 3-axis machining .
Prices vary significantly based on size and capability. Entry-level desktop models range from $45,000 to $75,000, while industrial machines cost between $120,000 and $250,000 . Mid-range options ($85,000-$110,000) now offer much of the precision of industrial units. Beyond the machine cost, buyers should budget for CAM software ($5k-$15k), specialized tooling, and operator training .
Yes, for complex parts requiring multiple setups on 3-axis machines. A 5-axis machine can reduce setups by up to 80%, cutting production time and labor costs significantly . It delivers better surface finishes, longer tool life through optimal cutting angles, and higher precision by eliminating repositioning errors . For high-value components like medical implants, aerospace parts, or complex molds, the investment typically pays for itself through improved efficiency and reduced scrap rates.
The main disadvantages are higher initial investment (2.5-4x more than 3-axis machines), programming complexity requiring advanced CAM software and skilled operators, and expensive maintenance . Collision risks are greater and harder to predict, requiring sophisticated simulation software . Additionally, tool radius compensation is not available in 5-axis mode, meaning different tool sizes require regenerated toolpaths . Workpiece size may also be limited by rotary table configurations .
Common mistakes include insufficient CAM simulation leading to collisions, incorrect post-processor selection causing machine errors, and inadequate fixturing that allows workpiece movement during complex rotations . Many operators underestimate programming complexity or purchase machines without verifying simultaneous 5-axis capability versus simpler 3+2 positioning . Poor thermal management and neglecting regular maintenance of rotary axes also lead to accuracy degradation over time .
With proper maintenance, a quality 5-axis machine typically lasts 10-15 years in production environments. Regular lubrication of linear guides and ball screws, electrical inspections, and spindle bearing maintenance can extend life by 3-5 years . Machines with premium components like P-grade linear guides and C3 ball screws maintain accuracy longer . The lifespan depends heavily on operating hours, materials machined, and adherence to manufacturer maintenance schedules.
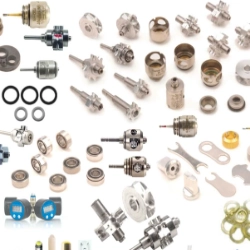
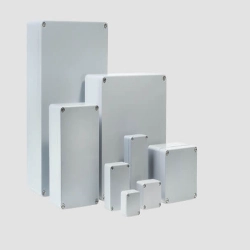
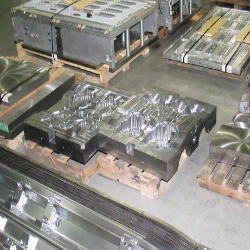
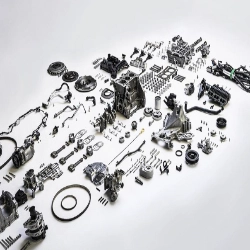
5-axis machines produce complex parts including aerospace turbine blades and structural components, medical implants (titanium knee joints, dental prosthetics), automotive engine components and prototypes, intricate mold and die sets with deep cavities, and precision electronic housings . They excel at parts requiring compound angles, organic freeform surfaces, undercuts, and features needing access from multiple sides—all completed in one clamping .
4-axis machining adds one rotary axis (typically A-axis) to standard 3-axis motion, allowing indexed rotation for machining multiple faces of prismatic parts . 5-axis machining adds two rotary axes for continuous simultaneous movement, enabling complex freeform surfaces, deep cavities, and compound angles . While 4-axis suits parts with features around a central axis, 5-axis is required for organic shapes, turbine blades, and parts needing constant tool angle adjustment . 5-axis reduces setups further but demands more complex programming and higher investment .